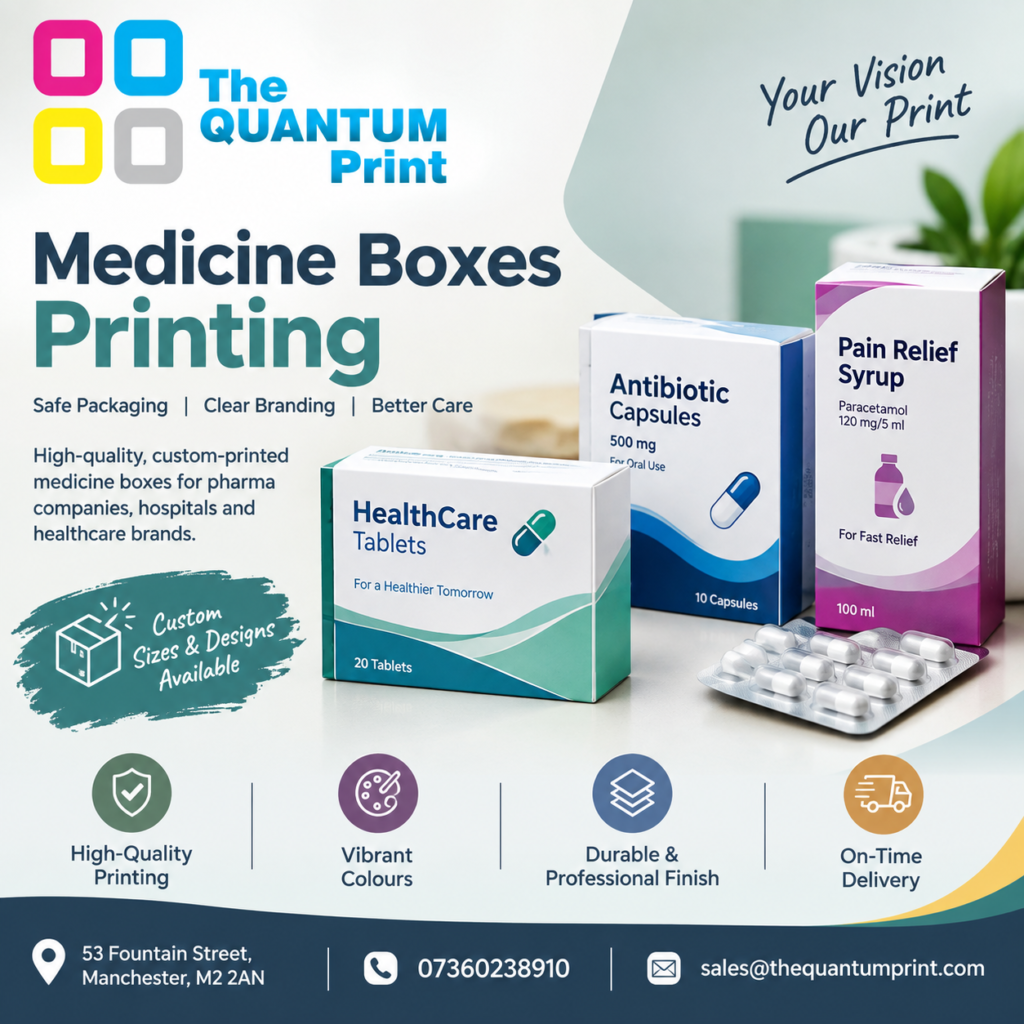
Packaging plays an important role in the pharmaceutical and healthcare sectors. A medicine box is not simply an outer container; it can help protect the product, communicate essential information, support brand recognition, and make handling easier throughout the supply chain. As healthcare packaging requirements become more sophisticated, businesses are paying greater attention to materials, printing quality, structural design, and information clarity.
For pharmaceutical brands, pharmacies, supplement manufacturers, and healthcare businesses in the UK, choosing suitable Medicine Boxes Printing solutions requires consideration of both presentation and practical requirements. The right packaging approach should balance durability, readability, compliance considerations, and efficient production.
Why Medicine Packaging Boxes Matter
Medicine packaging has several functions beyond containing a product. During transportation and storage, the box may need to withstand compression, friction, moisture exposure, and repeated handling. At the same time, the printed surface needs to remain clear enough for important product information to be identified.
Well-planned Medicine Packaging Boxes can support:
- Protection against ordinary handling and transportation damage
- Clear presentation of product information
- Consistent brand identification across product ranges
- Easier storage and organisation
- Tamper-evident or security-oriented structural features where appropriate
- Efficient use of shelf and warehouse space
Packaging design should therefore begin with the product’s practical requirements rather than focusing solely on appearance.
Key Considerations for Medicine Box Packaging
When developing medicine box packaging, businesses should consider the product dimensions, weight, distribution method, storage environment, and intended customer experience.

Material selection is one of the first decisions. Folding carton board is widely used for secondary pharmaceutical packaging because it can provide a practical combination of rigidity, printability, and efficient storage. The appropriate board specification depends on the size and weight of the contents and the structural design.
Printing is another important consideration. A medicine packaging box may contain information such as the product name, dosage instructions, ingredients, warnings, storage guidance, batch information, expiry details, and other required information. Typography should therefore prioritise readability over decorative complexity.
Colour can also have a functional role. Consistent colour systems can help distinguish different products or strengths within a range, provided the approach does not interfere with required information or create confusion.
Printing and Design Best Practices
Modern Medicine Boxes Printing can incorporate a variety of techniques to create clear and professional packaging. However, more printing effects do not necessarily mean better packaging. The most effective designs usually maintain a clear hierarchy of information.
Useful design practices include:
- Prioritise readability: Use appropriate font sizes, spacing, and contrast.
- Create a consistent hierarchy: Important product information should be easy to locate.
- Check artwork carefully: Spelling, dosage information, barcodes, symbols, and other details should be reviewed before production.
- Consider structural dimensions: The printed artwork must correspond accurately with the dieline and folding points.
- Allow for product differentiation: Different medicines or variants may require visually distinct packaging systems.
- Review colour consistency: Production samples or proofs can help identify colour differences before a larger print run.
For businesses developing several products, creating a consistent packaging system can also simplify future artwork updates and product extensions.
Common Challenges and Practical Solutions
Pharmaceutical packaging projects can face several recurring challenges. One is balancing the amount of information required on the packaging with limited surface area. Poor information hierarchy can make a box difficult to read even when all required details are technically present.

A practical solution is to organise information into clearly defined sections and use typography consistently. Important information should not be crowded by decorative graphics.
Another challenge is maintaining consistency across multiple production batches. Differences in materials, printing processes, or colour specifications can affect the finished appearance. Establishing clear artwork specifications and reviewing proofs can reduce avoidable inconsistencies.
Packaging waste is another growing consideration. Businesses are increasingly examining material efficiency and the overall lifecycle of packaging. Right-sizing a box can reduce unnecessary material use while also improving transport efficiency. However, structural reductions should never compromise the protection required by the product.
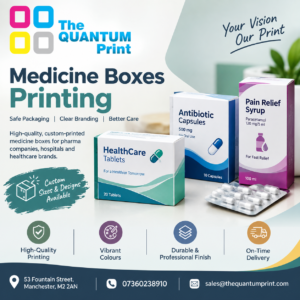
The Quantum Print provides an example of a UK packaging provider offering dedicated pharmaceutical-style box packaging solutions, demonstrating how specialised packaging formats can be developed around specific product requirements.
Applications and Emerging Trends
Medicine packaging is used across a broad range of healthcare applications, including prescription products, over-the-counter medicines, vitamins, supplements, medical products, and related healthcare goods.
A notable trend is the increasing use of packaging features that improve traceability and information access. Depending on the product and regulatory requirements, packaging may incorporate barcodes, serialisation-related information, QR codes, or other digital identifiers.
Sustainability is another area receiving increased attention. Businesses are examining recyclable paperboard options, responsible material sourcing, reduced packaging volume, and efficient production methods. The challenge is to introduce these improvements without compromising the protection, information clarity, or functional performance required from pharmaceutical packaging.

For businesses researching medicine box printing, it is useful to consider the entire packaging lifecycle rather than focusing only on the printed appearance. Material selection, structural design, artwork accuracy, production consistency, storage, transportation, and end-of-life considerations can all affect the final result.
Final Takeaway
Effective pharmaceutical packaging combines protection, communication, functionality, and visual consistency. Medicine Packaging Boxes need to accommodate practical product requirements while presenting essential information in a clear and organised way.
Whether a business is developing a new healthcare product or updating an existing packaging range, careful planning can prevent common problems such as incorrect dimensions, poor readability, inconsistent colours, and unnecessary material use. By treating packaging as part of the wider product experience rather than simply an outer container, businesses can create solutions that are practical, informative, and suitable for modern healthcare supply chains.